good manufacturing practice

Understanding Pharmaceutical Manufacturing Processes

Dr. John Smith

CA, USA


Introduction

Every tablet, capsule, injection, or syrup a patient takes is the result of a tightly controlled, multi-stage manufacturing process. Unlike many consumer goods, medicines must deliver the right amount of active ingredient, in the right form, every time, and small deviations can affect safety and efficacy. Pharmaceutical manufacturing is therefore as much a discipline of quality and control as it is of chemistry and engineering.

This article walks through the main stages of pharmaceutical manufacturing, from sourcing raw materials to releasing the finished product. It also explains the quality frameworks that govern these processes and the trends reshaping the industry.


1. The Big Picture: From Molecule to Medicine

Pharmaceutical manufacturing can be divided into two broad phases:

  1. Primary manufacturing, which produces the active pharmaceutical ingredient (API), also called the drug substance. This happens through chemical synthesis, fermentation, extraction from natural sources, or biotechnological processes using living cells.
  2. Secondary manufacturing, which converts the API into a finished dosage form (the drug product), such as tablets, capsules, liquids, creams, or injectables, and packages it for distribution.

Around both phases sits a quality system covering raw material testing, in-process controls, validation, documentation, and final release. The guiding principle is that quality cannot be tested into a product. It must be built into the process by design.


2. Product Development and Technology Transfer

Before commercial manufacturing begins, a product passes through development. Formulation scientists study the API’s physical and chemical properties, including solubility, particle size, polymorphism, stability, and compatibility with excipients (the inactive ingredients). These studies determine which dosage form is feasible and what manufacturing route will produce it consistently.

Modern development follows the Quality by Design (QbD) approach described in ICH Q8. Developers begin by defining a Quality Target Product Profile (QTPP), which sets out the intended characteristics of the final product. From it they identify Critical Quality Attributes (CQAs), such as assay, dissolution, content uniformity, and impurity levels. They then determine which Critical Material Attributes (CMAs) and Critical Process Parameters (CPPs) influence those attributes. Experiments, often using Design of Experiments (DoE), establish a design space: the range of input variables within which quality is assured.

Once a process is developed at laboratory and pilot scale, it undergoes technology transfer to the commercial site. This step moves knowledge, specifications, analytical methods, and process understanding from the development team to manufacturing, and it is a frequent source of scale-up problems. A well-documented transfer reduces the risk of failed batches and regulatory delays.


3. Raw Materials and Supplier Control

The quality of a medicine begins with its ingredients. Manufacturers source APIs, excipients, solvents, and packaging components from qualified suppliers, and each supplier goes through an approval process that may include audits, questionnaires, and sample testing.

On receipt, materials are:

  • Quarantined until tested and approved.
  • Sampled using statistically justified plans.
  • Tested against approved specifications for identity, purity, and other relevant attributes.
  • Labeled and stored under defined conditions of temperature, humidity, and light.

Only released materials may be used in production. Identity testing is especially important because supply chain mix-ups and adulteration have caused serious public health incidents in the past.


4. Manufacturing the Active Pharmaceutical Ingredient

Chemical Synthesis

Most small-molecule drugs are made through multi-step organic synthesis. Starting materials react in a controlled sequence to build the target molecule, with intermediates isolated and tested along the way. Key unit operations include:

  • Reaction: controlled addition of reagents, catalysts, and solvents in reactors, with attention to temperature, pressure, and mixing.
  • Separation and extraction: removing by-products and unreacted materials.
  • Crystallization: forming the solid API with the desired particle size and crystal form (polymorph).
  • Filtration and drying: isolating and removing residual solvents.
  • Milling and micronization: adjusting particle size, which can strongly affect dissolution and bioavailability.

Impurity control is central. Regulators expect manufacturers to identify, quantify, and limit organic impurities, residual solvents, and elemental impurities in line with ICH Q3A through Q3D.

Biotechnological APIs

Biologics such as monoclonal antibodies, vaccines, and recombinant proteins are produced by living systems, typically mammalian cells, bacteria, or yeast. The process has two main stages:

  • Upstream processing: growing cells in bioreactors under controlled conditions so they express the desired protein.
  • Downstream processing: harvesting, purifying (through chromatography and filtration), and formulating the product, including viral clearance steps where required.

Because biologics are large, complex molecules, the process largely defines the product. Even small changes in cell culture conditions can alter the final molecule’s characteristics.

ICH Q7 provides the GMP framework for APIs and is widely recognized as the international standard for API manufacturing.


5. Manufacturing the Finished Dosage Form

Oral Solid Dosage Forms

Tablets and capsules remain the most common dosage forms. A typical tablet process includes:

  1. Dispensing and weighing: each material is weighed and verified, often with a second-person check or an electronic system.
  2. Sieving and milling: ensuring uniform particle size and breaking up lumps.
  3. Blending: mixing the API and excipients to achieve content uniformity.
  4. Granulation: converting powder into granules to improve flow and compressibility. Wet granulation uses a liquid binder followed by drying. Dry granulation uses roller compaction. Direct compression skips granulation when the blend flows and compresses well enough on its own.
  5. Compression: forming tablets on a rotary press, with weight, hardness, thickness, and friability monitored.
  6. Coating: applying a film coat for taste masking, protection, appearance, or modified release.
  7. Capsule filling: for capsules, filling powder, granules, or pellets into hard gelatin or other shells.

Finished tablets are tested for dissolution, disintegration, assay, and content uniformity.

Liquid Oral Dosage Forms

Syrups, suspensions, and solutions involve dissolving or dispersing the API in a vehicle, along with preservatives, sweeteners, flavors, and buffers. Critical controls include mixing order, temperature, pH, viscosity, and microbial quality. Suspensions also require attention to particle settling and redispersibility.

Semi-Solid Dosage Forms

Creams, ointments, and gels are made by heating and combining oil and water phases, often with emulsifiers, then homogenizing and cooling under controlled conditions. Rheology, droplet size, and homogeneity are key quality attributes.

Sterile Products

Injectables, ophthalmic preparations, and some other products must be sterile. Sterile manufacturing is among the most demanding areas of the industry and follows one of two routes:

  • Terminal sterilization: the product is filled and sealed, then sterilized in its final container, usually by steam (autoclave). This is preferred when the product can tolerate heat.
  • Aseptic processing: the product and its container components are sterilized separately, then filled and sealed in an aseptic environment. This is used for heat-sensitive products, including many biologics.

Aseptic manufacturing requires classified cleanrooms, unidirectional airflow, rigorous gowning, environmental monitoring, and media fill simulations that demonstrate the process can maintain sterility. Increasingly, manufacturers use isolators and restricted access barrier systems (RABS) to separate operators from the product. The revised EU GMP Annex 1 (2022) emphasizes a holistic Contamination Control Strategy for sterile manufacturing.

Lyophilization (freeze-drying) is used for products unstable in solution. It removes water by sublimation under vacuum, yielding a stable powder for reconstitution.


6. Packaging and Labeling

Packaging is not an afterthought. It protects the product from moisture, oxygen, and light, and it carries the information patients and clinicians depend on. Packaging operations include:

  • Primary packaging: blisters, bottles, vials, ampoules, syringes, or sachets in direct contact with the product.
  • Secondary packaging: cartons, leaflets, and shipping cases.
  • Labeling and serialization: printing batch numbers, expiry dates, and, increasingly, unique identifiers to combat counterfeiting and support traceability.

Mix-ups are a major risk here. Controls such as line clearance, label reconciliation, automated vision inspection, and barcode verification prevent the wrong label or leaflet from reaching the wrong product. Packaging is also studied for compatibility with the product through stability testing under ICH Q1A conditions.


7. Quality Control, Quality Assurance, and Batch Release

Quality Control (QC) and Quality Assurance (QA) work together but have distinct roles.

Quality Control performs the testing: raw material analysis, in-process checks, finished product testing, stability studies, and microbiological and environmental monitoring. Analytical methods must be validated for accuracy, precision, specificity, linearity, and robustness (ICH Q2).

Quality Assurance oversees the overall system. It reviews batch records, approves procedures, manages deviations, change control, and corrective and preventive actions (CAPA), conducts internal audits, and ultimately authorizes batch release.

Before a batch is released, QA reviews the complete batch manufacturing record, confirms all tests met specifications, verifies that any deviations were investigated and closed, and checks that the process ran within validated parameters. Only then is the product released for distribution.


8. Process Validation and Cleaning Validation

Process validation provides documented evidence that a process consistently produces a product meeting its predetermined specifications. The modern lifecycle approach, described in regulatory guidance, has three stages:

  1. Process design: defining the commercial process based on development knowledge.
  2. Process qualification: confirming the process performs as intended at commercial scale, including qualification of facilities, utilities, and equipment.
  3. Continued process verification: ongoing monitoring during routine production to confirm the process remains in a state of control.

Cleaning validation addresses cross-contamination in multi-product facilities. Manufacturers must show that cleaning procedures reliably remove product residues, cleaning agents, and microbial contamination to acceptable limits. These limits are increasingly based on toxicological assessments, such as health-based exposure limits.


9. Facilities, Utilities, and Equipment

The manufacturing environment is part of the process. Good facility design supports logical material and personnel flow, prevents cross-contamination, and allows effective cleaning. Key elements include:

  • HVAC systems that control air quality, pressure differentials, temperature, and humidity.
  • Water systems: purified water and Water for Injection (WFI) are critical utilities, continuously monitored for conductivity, total organic carbon, and microbial counts.
  • Compressed gases and steam that contact the product or equipment and must meet quality standards.
  • Qualified equipment: installation, operational, and performance qualification (IQ/OQ/PQ), combined with preventive maintenance and calibration.

10. Documentation and Data Integrity

In pharmaceutical manufacturing the saying goes, “If it isn’t documented, it didn’t happen.” Master formulas, batch records, standard operating procedures, logbooks, and test records form the evidence trail that demonstrates compliance.

Regulators place strong emphasis on data integrity, commonly summarized by the ALCOA+ principles: data should be Attributable, Legible, Contemporaneous, Original, and Accurate, as well as Complete, Consistent, Enduring, and Available. Electronic systems require audit trails, access controls, and validation to ensure records are trustworthy.


11. Regulatory Oversight and Quality Risk Management

Manufacturers operate under GMP regulations enforced by authorities such as the US FDA, the European Medicines Agency and national EU authorities, the UK MHRA, and many others, with harmonization efforts through ICH, WHO, and PIC/S. Regular inspections verify compliance, and serious findings can lead to warning letters, import bans, or product recalls.

Quality Risk Management (ICH Q9) gives a systematic way to assess and control risks to product quality. Tools such as Failure Mode and Effects Analysis (FMEA) and Hazard Analysis and Critical Control Points (HACCP) help companies focus resources on the highest-risk areas. ICH Q10 adds a model for a Pharmaceutical Quality System built on management responsibility and continual improvement.


12. Emerging Trends in Pharmaceutical Manufacturing

The industry is changing, driven by demands for efficiency, flexibility, and resilience.

Continuous manufacturing replaces traditional batch-by-batch production with an uninterrupted flow from raw materials to finished product. It can reduce footprint, shorten production time, and allow real-time quality monitoring.

Process Analytical Technology (PAT) uses in-line or at-line sensors, such as near-infrared spectroscopy, to monitor quality during production. This supports real-time release testing and reduces dependence on end-product testing.

Advanced therapies, including cell and gene therapies, require individualized, often small-scale manufacturing with tight timelines and complex logistics.

Digitalization and Industry 4.0 technologies, including manufacturing execution systems, electronic batch records, data analytics, and machine learning, improve traceability and help predict equipment issues before they cause failures.

3D printing is being explored for personalized dosing and complex release profiles.

Green chemistry and sustainability efforts aim to reduce solvent use, waste, and energy consumption across the lifecycle.


13. Common Challenges

Despite technological progress, manufacturers face persistent challenges:

  • Supply chain vulnerability: dependence on limited suppliers for critical materials can cause shortages.
  • Scale-up difficulties: processes that work in the lab may behave differently at commercial scale.
  • Contamination and cross-contamination: especially in multi-product facilities and sterile operations.
  • Regulatory complexity: requirements differ across regions, complicating global supply.
  • Skilled workforce: advanced processes require trained personnel with both technical and quality expertise.
  • Cost pressure: particularly for generics, where margins are thin but quality expectations are unchanged.

Addressing these requires a strong quality culture in which everyone, from operators to senior management, understands that patient safety comes first.


Conclusion

Pharmaceutical manufacturing combines science, engineering, and rigorous quality management. It begins with carefully controlled raw materials and API production, moves through formulation and dosage form manufacture, and ends with packaging, testing, and release, all under a system that documents every step. Concepts such as Quality by Design, process validation, risk management, and data integrity are the foundation of consistent product quality.

As continuous manufacturing, real-time monitoring, and digital tools mature, the industry is moving toward processes that are more efficient, more flexible, and better understood. Through all these changes the goal stays the same: delivering safe, effective, high-quality medicines to every patient, every time.


Guideline References

  1. ICH Q7 – Good Manufacturing Practice Guide for Active Pharmaceutical Ingredients.
  2. ICH Q8 (R2) – Pharmaceutical Development.
  3. ICH Q9 (R1) – Quality Risk Management.
  4. ICH Q10 – Pharmaceutical Quality System.
  5. ICH Q11 – Development and Manufacture of Drug Substances.
  6. ICH Q1A (R2) – Stability Testing of New Drug Substances and Products.
  7. ICH Q2 (R2) – Validation of Analytical Procedures.
  8. ICH Q3A–Q3D – Impurities: new drug substances and products, residual solvents, and elemental impurities.
  9. US FDA, 21 CFR Part 210 and Part 211 – Current Good Manufacturing Practice for Finished Pharmaceuticals.
  10. US FDA (2011) – Guidance for Industry: Process Validation: General Principles and Practices.
  11. European Commission, EudraLex Volume 4 – EU Guidelines for Good Manufacturing Practice for Medicinal Products for Human and Veterinary Use, including Annex 1 (Manufacture of Sterile Medicinal Products) and Annex 15 (Qualification and Validation).
  12. WHO Technical Report Series No. 986, Annex 2 – WHO Good Manufacturing Practices for Pharmaceutical Products: Main Principles.
  13. PIC/S PE 009 – Guide to Good Manufacturing Practice for Medicinal Products.
  14. PIC/S PI 041 and US FDA guidance on Data Integrity and Compliance with Drug CGMP.
  15. US FDA (2004) – Guidance for Industry: PAT, A Framework for Innovative Pharmaceutical Development, Manufacturing, and Quality Assurance.

Understanding Pharmaceutical Manufacturing Processes Read More »
Definition of GMP according to different Pharmaceutical guideline

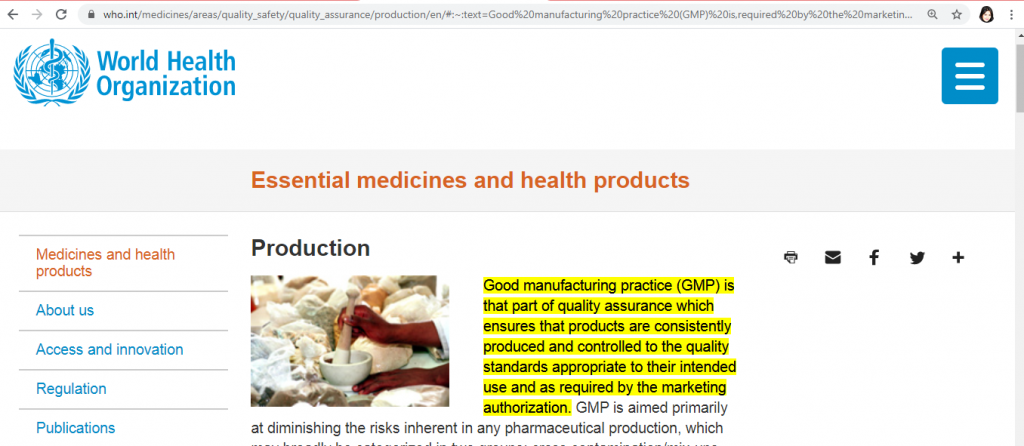
Definition of GMP according to WHO guideline

Definition of GMP: “Good manufacturing practice (GMP) is that part of quality assurance which ensures that products are consistently produced and controlled to the quality standards appropriate to their intended use and as required by the marketing authorization.”

definition of GMP


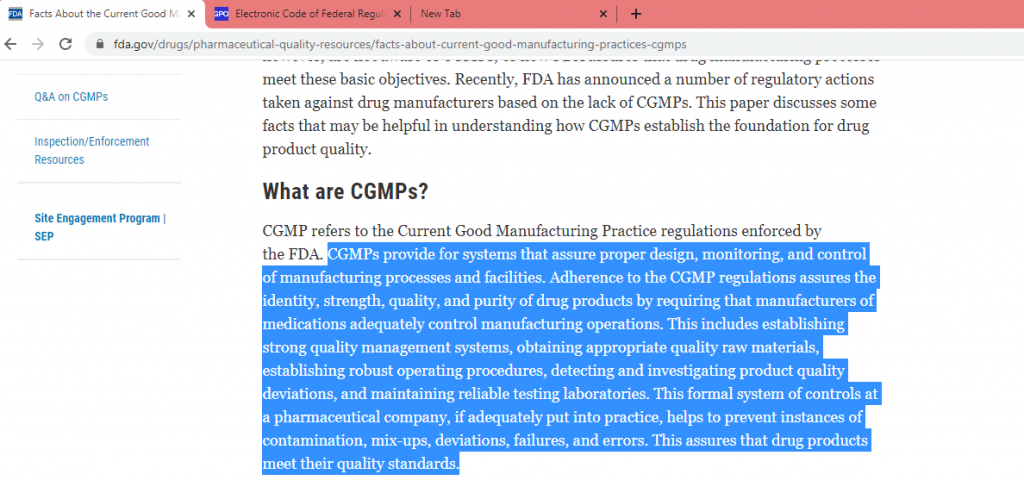
Definition of GMP according to US FDA Guideline

CGMPs provide for systems that assure proper design, monitoring, and control of manufacturing processes and facilities. Adherence to the CGMP regulations assures the identity, strength, quality, and purity of drug products by requiring that manufacturers of medications adequately control manufacturing operations. This includes establishing strong quality management systems, obtaining appropriate quality raw materials, establishing robust operating procedures, detecting and investigating product quality deviations, and maintaining reliable testing laboratories. This formal system of controls at a pharmaceutical company, if adequately put into practice, helps to prevent instances of contamination, mix-ups, deviations, failures, and errors. This assures that drug products meet their quality standards.

definition of GMP
 
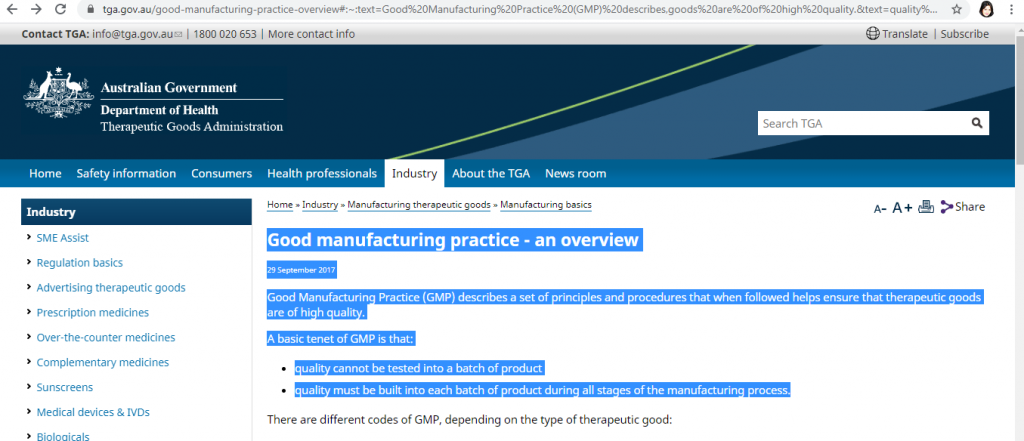
Definition of GMP according to TGA Guideline

“Good Manufacturing Practice (GMP) describes a set of principles and procedures that when followed helps ensure that therapeutic goods are of high quality. A basic tenet of GMP is that quality cannot be tested into a batch of product. Quality must be built into each batch of product during all stages of the manufacturing process”

definition of GMP
 
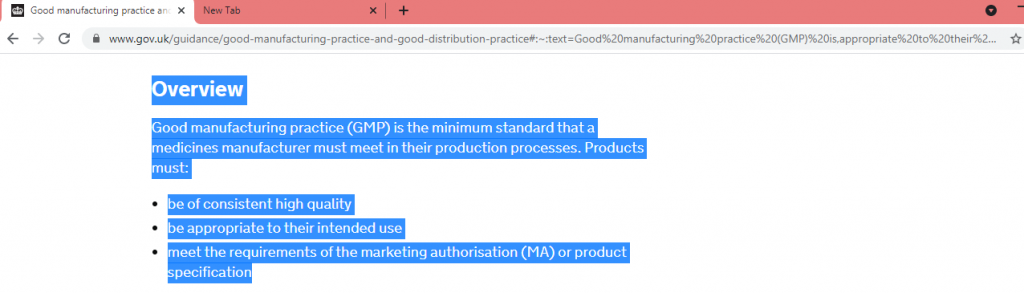
Definition of GMP according to UK MHRA guideline

Good manufacturing practice (GMP) is the minimum standard that a medicines manufacturer must meet in their production processes. Products must:

  • be of consistent high quality
  • be appropriate to their intended use
  • meet the requirements of the marketing authorisation (MA) or product specification
definition of GMP
According to WHO

“GMP covers all aspects of the manufacturing process: defined manufacturing process; validated critical manufacturing steps; suitable premises, storage, transport; qualified and trained production and quality control personnel; adequate laboratory facilities; approved written procedures and instructions; records to show all steps of defined procedures taken; full traceability of a product through batch processing records and distribution records; and systems for recall and investigation of complaints”.


What is GMP?

Good Manufacturing Practices (GMP) are a set of strict guidelines and principles used by pharmaceutical companies to ensure consistent production of safe, high-quality pharmaceutical products. These guidelines are important to maintain the integrity of manufacturing processes, maintain public health standards, and comply with regulatory requirements from global health authorities such as the U.S. Food and Drug Administration (FDA) or the European Medicines Agency (EMA). ) Europe. Below is a closer look at the key aspects of GMP in the pharmaceutical industry.


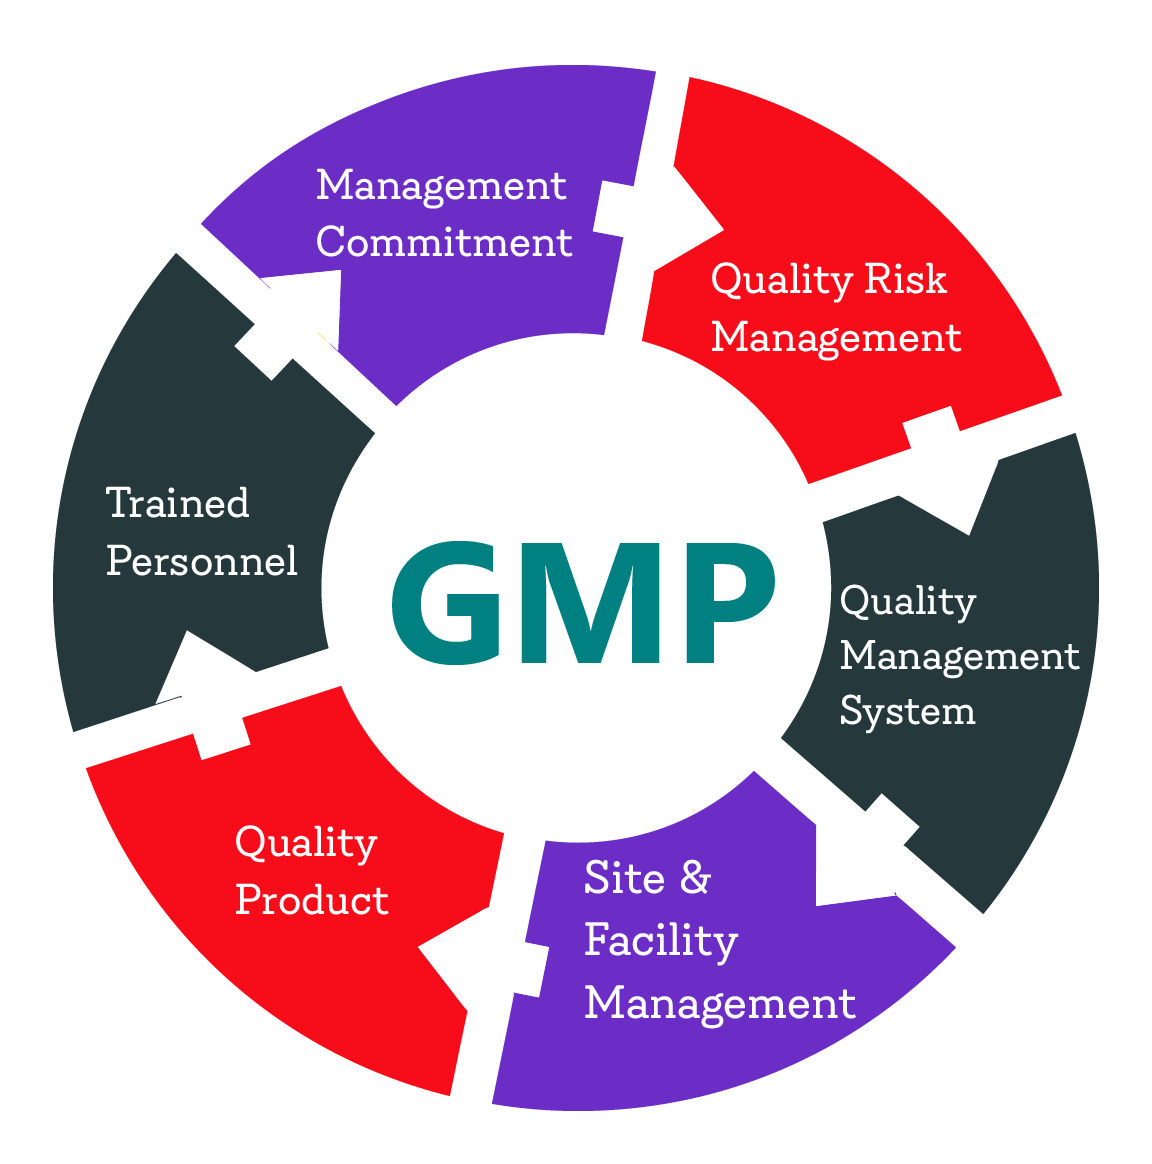
  • Documents and Records
  • Quality management system
  • Staff training
  • System and device maintenance
  • Validity and Acceptability
  • Raw material inspection
  • Process control
  • Quality control and testing
  • Traceability and withdrawal procedures
 
Documents and Records:

Complete and accurate documentation is critical to GMP. It includes detailed records of manufacturing processes, procedures and results. For example, pharmaceutical companies carefully record every step of the production of a particular drug, from raw material supply to final packaging.

Thorough and accurate documentation of good manufacturing practices (GMP) plays an important role. This involves carefully recording various aspects of production, including processes, procedures, and results. Take the pharmaceutical industry, for example, where pharmaceutical companies take great care to document every critical step in the production of a particular drug.

In compliance with GMP standards, the documentation process begins with detailed records of raw material procurement. Pharmaceutical companies carefully record information about the origin, quality, and quantity of each raw material used in the pharmaceutical manufacturing process. This documentation is not only essential for quality control, but also serves as the basis for traceability and allows the company to identify and correct any problems that arise during the production cycle.

Each step in pharmaceutical manufacturing is accurately documented as the manufacturing process progresses. This includes information about the equipment used, environmental conditions, and deviations from standard procedures. For example, if specific temperatures or pressures are important for a particular production step, these parameters are recorded to ensure consistency and reproducibility.

In addition to manufacturing processes, GMP documents also contain procedures that control various aspects of manufacturing. This includes standard operating procedures (SOPs) for equipment calibration, cleaning protocols, and employee training. Pharmaceutical companies ensure that these procedures are not only fully documented but also regularly updated to reflect improvements or changes in industry regulations.

Outcomes such as product quality and test results are also carefully documented within the GMP framework. Pharmaceutical companies keep detailed records of the quality control tests performed at various stages of manufacturing. This document is an important tool during regulatory investigations and demonstrates the company’s commitment to producing safe and effective medicines.


GMP documentation also extends to final packaging. From the materials used in packaging to the labeling process, every detail is recorded to ensure compliance with regulatory requirements and ensure the safety of end users. This comprehensive document will help you not only comply with regulatory standards, but also improve overall product quality and compliance.

In summary, the importance of complete and accurate documentation in the GMP area cannot be overemphasized. The pharmaceutical industry’s commitment to documenting all aspects of the manufacturing process, from raw material procurement to final packaging, not only ensures regulatory compliance, but also promotes a culture of continuous improvement, quality assurance, and accountability within the industry.

 
Quality management system

A robust quality control system is implemented to monitor all aspects of manufacturing, testing and quality control. This involves creating and maintaining processes to consistently produce pharmaceutical products that meet predetermined quality standards.


Establishing and maintaining a strong quality management system plays a critical role in ensuring complete oversight of all aspects of the manufacturing, analytical and quality control processes in the pharmaceutical industry. This system has been carefully designed to create a facility that consistently produces pharmaceutical products that meet stringent predetermined quality standards.

To better understand the importance of these systems, let us consider a real-world example from a pharmaceutical manufacturing plant. The introduction of a quality management system involves careful documentation and standardization of production processes. This includes everything from raw material collection and storage to the actual manufacturing process.

For example, if you produce life-saving pharmaceuticals, your quality management system establishes clear protocols for sourcing and verifying raw materials. This may include rigorous testing and certification processes to ensure the purity and integrity of ingredients used in pharmaceutical formulations.

Once the manufacturing process begins, quality control systems monitor each step to ensure compliance with predetermined standards. This may include real-time data monitoring, automated quality checks, and routine inspections to identify and address deviations from established protocols.

Testing is another important step and a quality management system ensures that rigorous testing procedures are implemented. This may include a variety of analytical techniques, such as chromatography or mass spectrometry, to test the structure and efficacy of the drug. The system also monitors environmental conditions such as temperature and humidity to ensure the stability and functionality of the final product.

Quality control measures within the system go beyond manufacturing and include aspects such as packaging and labeling. For example, in the pharmaceutical manufacturing case, quality control systems enforce standards for proper labeling, tamper-evident packaging, and verification of expiration dates to protect end users.

Regular audits and reviews are an essential part of this system. This allows you to continuously evaluate performance and identify areas for continuous improvement. By implementing a strong quality management system, pharmaceutical companies not only comply with regulatory requirements, but also build trust among consumers, healthcare professionals, and regulators regarding the safety and effectiveness of their products.

 
Staff training

GMP requires that all employees involved in the manufacturing process receive extensive training. This ensures that employees are fully familiar with the processes and requirements associated with their role. For example, people working in quality control must be trained to perform accurate and reliable testing on pharmaceutical products.

Compliance with Good Manufacturing Practices (GMP) requires in-depth training for all employees involved in the production process and emphasizes the importance of ensuring high levels of employee efficiency and performance. This rigorous training program aims to provide employees with a deep understanding of the specific procedures and requirements associated with their respective roles within a manufacturing facility.

For example, quality control personnel play a key role in ensuring compliance with GMP standards. Our extensive training program provides these individuals with the skills and knowledge necessary to perform accurate and reliable pharmaceutical testing. This includes training in the use of state-of-the-art testing equipment, adherence to established testing protocols, and the ability to accurately interpret and analyze test results.

The training not only covers technical aspects, but also emphasizes the importance of a strong awareness of quality standards and compliance. This comprehensive approach ensures that quality control personnel not only perform their duties properly, but also understand the broader context of GMP regulations and their role in ensuring the overall quality and safety of pharmaceutical products.

Additionally, GMP training goes beyond specific job functions to include broader concepts such as sanitation, documentation practices, and safety protocols. For example, production workers are trained in proper dressing procedures and hygiene practices to prevent contamination during manufacturing. Training programs may also include modules on documentation standards to ensure accurate records of all manufacturing activities, which are important for traceability and compliance.

By investing in extensive training, companies not only meet legal requirements, but also instill a culture of excellence and responsibility in their employees. In turn, this contributes to the overall reliability and integrity of the manufacturing process and ultimately promotes the quality and safety of the medicines delivered to consumers.


System and device maintenance

Regular maintenance of plant and equipment is essential to prevent contamination and maintain the accuracy of manufacturing processes. A practical example is planning regular inspection and maintenance of pharmaceutical manufacturing equipment to prevent defects that could affect product quality.

Regular maintenance of plant and equipment is essential to prevent contamination and maintain the accuracy of production processes. A prime example of this need is strategic planning for regular inspection and maintenance of machinery used in pharmaceutical manufacturing. Implementing a proactive maintenance approach allows you to quickly identify and resolve potential defects that could compromise the quality of the final product.

In the pharmaceutical industry, where precision and purity are top priorities, continuous operation of special equipment is very important. A regular maintenance routine, including thorough inspection and maintenance, becomes an essential part of a strong quality assurance system. For example, in pharmaceutical manufacturing plants, complex machinery such as tablet presses, mixers, and encapsulation machines must be inspected regularly to ensure they are operating within set parameters.

A practical example of the importance of regular maintenance can be seen through the example of a tablet press used to produce pharmaceutical tablets. Regular inspections include a complete inspection of machine components such as: B. Tools, pressure rollers and feeding systems. Maintenance activities include lubrication, calibration, and replacement of worn parts.

Following a proactive maintenance plan can help you identify potential problems early, such as wear, deformation or risk of contamination. Resolving these issues in a timely manner helps prevent unexpected errors and reduce downtime in the manufacturing process. This not only ensures consistent quality of medicines, but also contributes to operational efficiency and cost-effectiveness.


In essence, proactive maintenance of plant and equipment, including through regular inspections and maintenance, plays a key role in the pharmaceutical manufacturing process. This approach not only protects against contamination, but also ensures the precision needed to maintain the highest product quality in industries where reliability and compliance are paramount.

 
Validity and Acceptability

GMP requires verification and qualification of equipment, processes and systems to ensure efficiency and consistency. For example, pharmaceutical companies can ensure that a particular manufacturing process consistently produces drugs that meet required specifications.

Good Manufacturing Practices (GMP) require a thorough verification and qualification process of equipment, processes and systems to ensure efficiency and consistency. These rigorous verifications ensure that our manufacturing operations meet established standards and consistently deliver high-quality products.

For example, consider a pharmaceutical company that produces drugs. By adhering to GMP principles, the company will control preventive measures in certain manufacturing processes. This validation process includes extensive testing and analysis to ensure that the manufacturing process consistently produces medicines that meet regulatory authorities’ rigorous specifications and quality standards.

During this validation process, pharmaceutical companies carefully evaluate various parameters such as raw material specifications, device performance, environmental conditions, and process controls. The goal is to provide evidence and documentation that the manufacturing process consistently produces a drug with the desired properties, ensuring safety, efficacy, and quality of the final product.

Moreover, this verification process is more than an isolated event. It is a constant effort to continuously improve. Regular assessments, redesigns and updates ensure good processes remain effective and aligned with evolving industry standards. This proactive approach not only ensures GMP compliance, but also increases the overall efficiency and reliability of pharmaceutical manufacturing, helping to deliver safe and effective medicines to consumers.

 
Raw material inspection

We apply rigorous procedures to check and test our raw materials to ensure they meet our quality specifications. In fact, pharmaceutical manufacturers can test the purity, potency, and other relevant characteristics of incoming raw materials before incorporating them into the manufacturing process.
Strict protocols are in place to control and test raw materials to ensure stringent quality specifications are met. A great example of this delicate process can be seen in the pharmaceutical industry, where manufacturers carefully test incoming raw materials for a variety of important characteristics such as purity and potency. These raw materials undergo extensive testing to ensure they meet the highest standards before being incorporated into the manufacturing process.

Implementing robust testing procedures in pharmaceutical manufacturing requires evaluating raw materials against predetermined criteria to ensure quality and suitability for use. For example, pharmaceutical companies may use advanced analytical techniques such as chromatography or spectroscopy to analyze the purity of compounds in their raw materials. This ensures that the ingredients meet the required specifications and do not contain impurities that could compromise the safety and functionality of the final product.


Moreover, efficacy testing is an important aspect of the evaluation process, especially for drugs where precise dosing is important for therapeutic efficacy. Manufacturers can accurately measure the active ingredients in their raw materials using sophisticated methods such as high-performance liquid chromatography (HPLC) or mass spectrometry.

In addition to assessing purity and potency, other relevant characteristics such as particle size, moisture content, and microbial contamination can also be examined in depth. This multi-layered approach ensures a complete evaluation of raw materials and does not allow for any compromise in the quality of the final drug product.

By implementing these rigorous testing procedures, pharmaceutical manufacturers not only comply with legal requirements, but also emphasize the production of safe, high-quality drugs. Effective control and analysis systems are essential to ensure that raw materials used in the pharmaceutical industry meet the high standards required to develop reliable and effective medical solutions.

 
Process control

GMP emphasizes implementing controls at various stages of the manufacturing process to ensure consistency and quality. This may involve monitoring critical process parameters in real time to immediately detect and correct deviations.
Good manufacturing practices (GMP) place great importance on the careful application of stringent controls throughout the manufacturing process to ensure consistency and high quality of the final product. This comprehensive approach includes continuous real-time monitoring of critical process parameters, allowing deviations from set values to be immediately detected and corrected.

For example, in the pharmaceutical industry, GMP compliance is essential to ensure safe and effective drug production. Various critical parameters such as drug preparation time, temperature, pressure, and chemical concentration are monitored in real time. If any of these parameters fall outside the specified range, the automated system will raise an alert so operators can take immediate action to correct the problem. This proactive monitoring and timely corrective action not only ensures product quality, but also contributes to the overall safety and efficacy of medicines that reach consumers.

In the context of food manufacturing, GMP practices include monitoring issues such as hygiene, temperature, and ingredient ratios. For example, in packaged food production, strict control measures are implemented to maintain hygiene standards at all stages of the production process. Automatic sensors continuously monitor cleaning and, if there are any deviations, initiate an automatic cleaning process to ensure that the end product meets the highest quality and safety standards.

The application of GMP principles extends beyond the pharmaceutical and food industries to a variety of industries, including electronics, cosmetics, and automobile manufacturing. In any case, real-time monitoring of critical parameters and prompt corrective action demonstrates commitment to GMP and ensures consistent production of high-quality products across a variety of industries.

 
Quality control and testing

Intermediate and final products undergo rigorous quality control and testing to ensure they meet specified specifications. This includes extensive testing for aspects such as purity, stability and dissolution rate.

Extensive testing and quality control procedures are systematically implemented throughout the manufacturing process, covering both intermediate and final products. The main purpose is to ensure that these products meet strict quality standards by ensuring that they meet specific specifications. Our testing program is comprehensive and focuses on critical factors such as purity, stability, and dissolution rate that are critical to the overall quality and effectiveness of the end result.

For example, in pharmaceutical manufacturing, intermediate products undergo rigorous testing to assess their chemical purity and ensure that they meet the required pharmacological standards. Stability testing determines a product’s resistance to various environmental conditions, ensuring its effectiveness throughout its shelf life. Additionally, dissolution rate testing is very important, especially for oral drugs. This is because it directly influences treatment results by assessing the amount and speed at which active ingredients are released into the body.

In the electronics industry, strict quality control is applied to final products such as smartphones. Purity testing of electronic components ensures that they meet specified standards, preventing defects or performance issues. Reliability testing is essential to ensure that devices can withstand a variety of environmental conditions without performance degradation. Additionally, testing battery discharge rates ensures consistent and stable power delivery over time, improving the overall reliability of the product.

These examples demonstrate how rigorous quality control and testing processes are essential in a variety of industries to ensure that intermediate and final products always meet specified specifications and ultimately increase customer satisfaction and product reliability.

 
Traceability and withdrawal procedures

GMP requires the establishment of a traceability system to track and recall products in case of quality issues or regulatory violations. Real-world examples include implementing a barcode system to easily identify and recall products in the event of a recall.

Compliance with GMP in the pharmaceutical industry is not only a regulatory requirement, but also a critical factor in protecting public health and maintaining the reputation of pharmaceutical companies. Practical implementation of GMP principles allows careful control of all stages of pharmaceutical production to produce safe and consistently high-quality products.

Good Manufacturing Practices (GMP) mandate the creation of a robust traceability system to monitor and recover products if quality issues occur or deviations from compliance standards occur. A specific example of this need is the integration of advanced barcoding systems into pharmaceutical production processes. This implementation allows for seamless product identification and recovery in recall situations and increases the efficiency and accuracy of the overall process.

Imagine a pharmaceutical company that diligently applies GMP principles to its operations. The company uses cutting-edge barcode technology as part of its tracking system. Each product is assigned a unique barcode, linked to extensive data about production details, ingredients and quality control systems. If there is a quality or non-compliance issue, these barcodes are essential to quickly identify and isolate affected batches.

What is cGMP

To delve deeper into the practical significance, imagine a situation where a particular batch of medicine is suspected to be out of quality standards. GMP-compliant tracking systems allow companies to quickly identify affected products by scanning barcodes, allowing batches to be quickly removed from distribution channels, preventing potential loss to customers. Detailed data associated with the barcode can help you find the root cause of the problem and implement corrective actions to prevent the problem from recurring.

In essence, GMP compliance in the pharmaceutical industry goes beyond regulatory obligations. This is proving to be an important factor in maintaining public health and strengthening the reputation of pharmaceutical companies. Practical implementation of GMP principles, such as the use of advanced tracking systems such as barcodes, implies a commitment to strict control at all stages of the production process. These efforts result in the production of safe, consistent, high-quality medicines that not only ensure regulatory compliance but, more importantly, increase consumer trust and maintain the integrity of the industry.

Definition of GMP according to different Pharmaceutical guideline Read More »